Execute a Meticulous Cost-Benefit Analysis for Pump Replacement
The financial calculus of an aerobic septic pump replacement extends beyond the initial hardware acquisition. A comprehensive analysis must account for labor, system-specific components, and potential secondary failures. The initial investment in a high-quality pump mitigates long-term operational expenditures. Below is a detailed cost matrix based on industry averages and component specifications. Note that costs can fluctuate based on regional labor rates and supply chain logistics, particularly for specialized pump models required for specific Total Dynamic Head (TDH) calculations. Keeping your system healthy is easier when you partner with top-rated South Miami, FL septic technicians.
| Component / Service | Typical Cost Range (USD) | Technical Justification & Notes |
|---|---|---|
| Submersible Effluent Pump (Pump Only) | $450 – $900 | Cost varies by horsepower (HP), GPM rating, and materials (e.g., cast iron vs. thermoplastic). Cast iron housing is superior for heat dissipation. |
| Aerator Pump / Air Compressor | $400 – $850 | Linear diaphragm and rotary vane are common types. Diaphragm kits are a frequent replacement item (approx. $80-150). |
| Professional Labor | $300 – $700 | Includes pump extraction, new pump installation, electrical connection verification, and operational testing. Typically 2-4 hours for a licensed technician. |
| Float Switch Assembly Replacement | $150 – $350 | Often replaced concurrently with the pump. Failure to do so is a primary cause of premature new pump failure (either burnout or short-cycling). |
| Control Panel Diagnostics/Repair | $200 – $600+ | May involve replacing relays, timers, or circuit breakers that were damaged by the initial pump failure’s electrical fault. |
| Total Estimated Project Cost | $900 – $2,500+ | The final figure is contingent on the scope of component failure and system complexity. |

Analyze This Real-World Failure Scenario
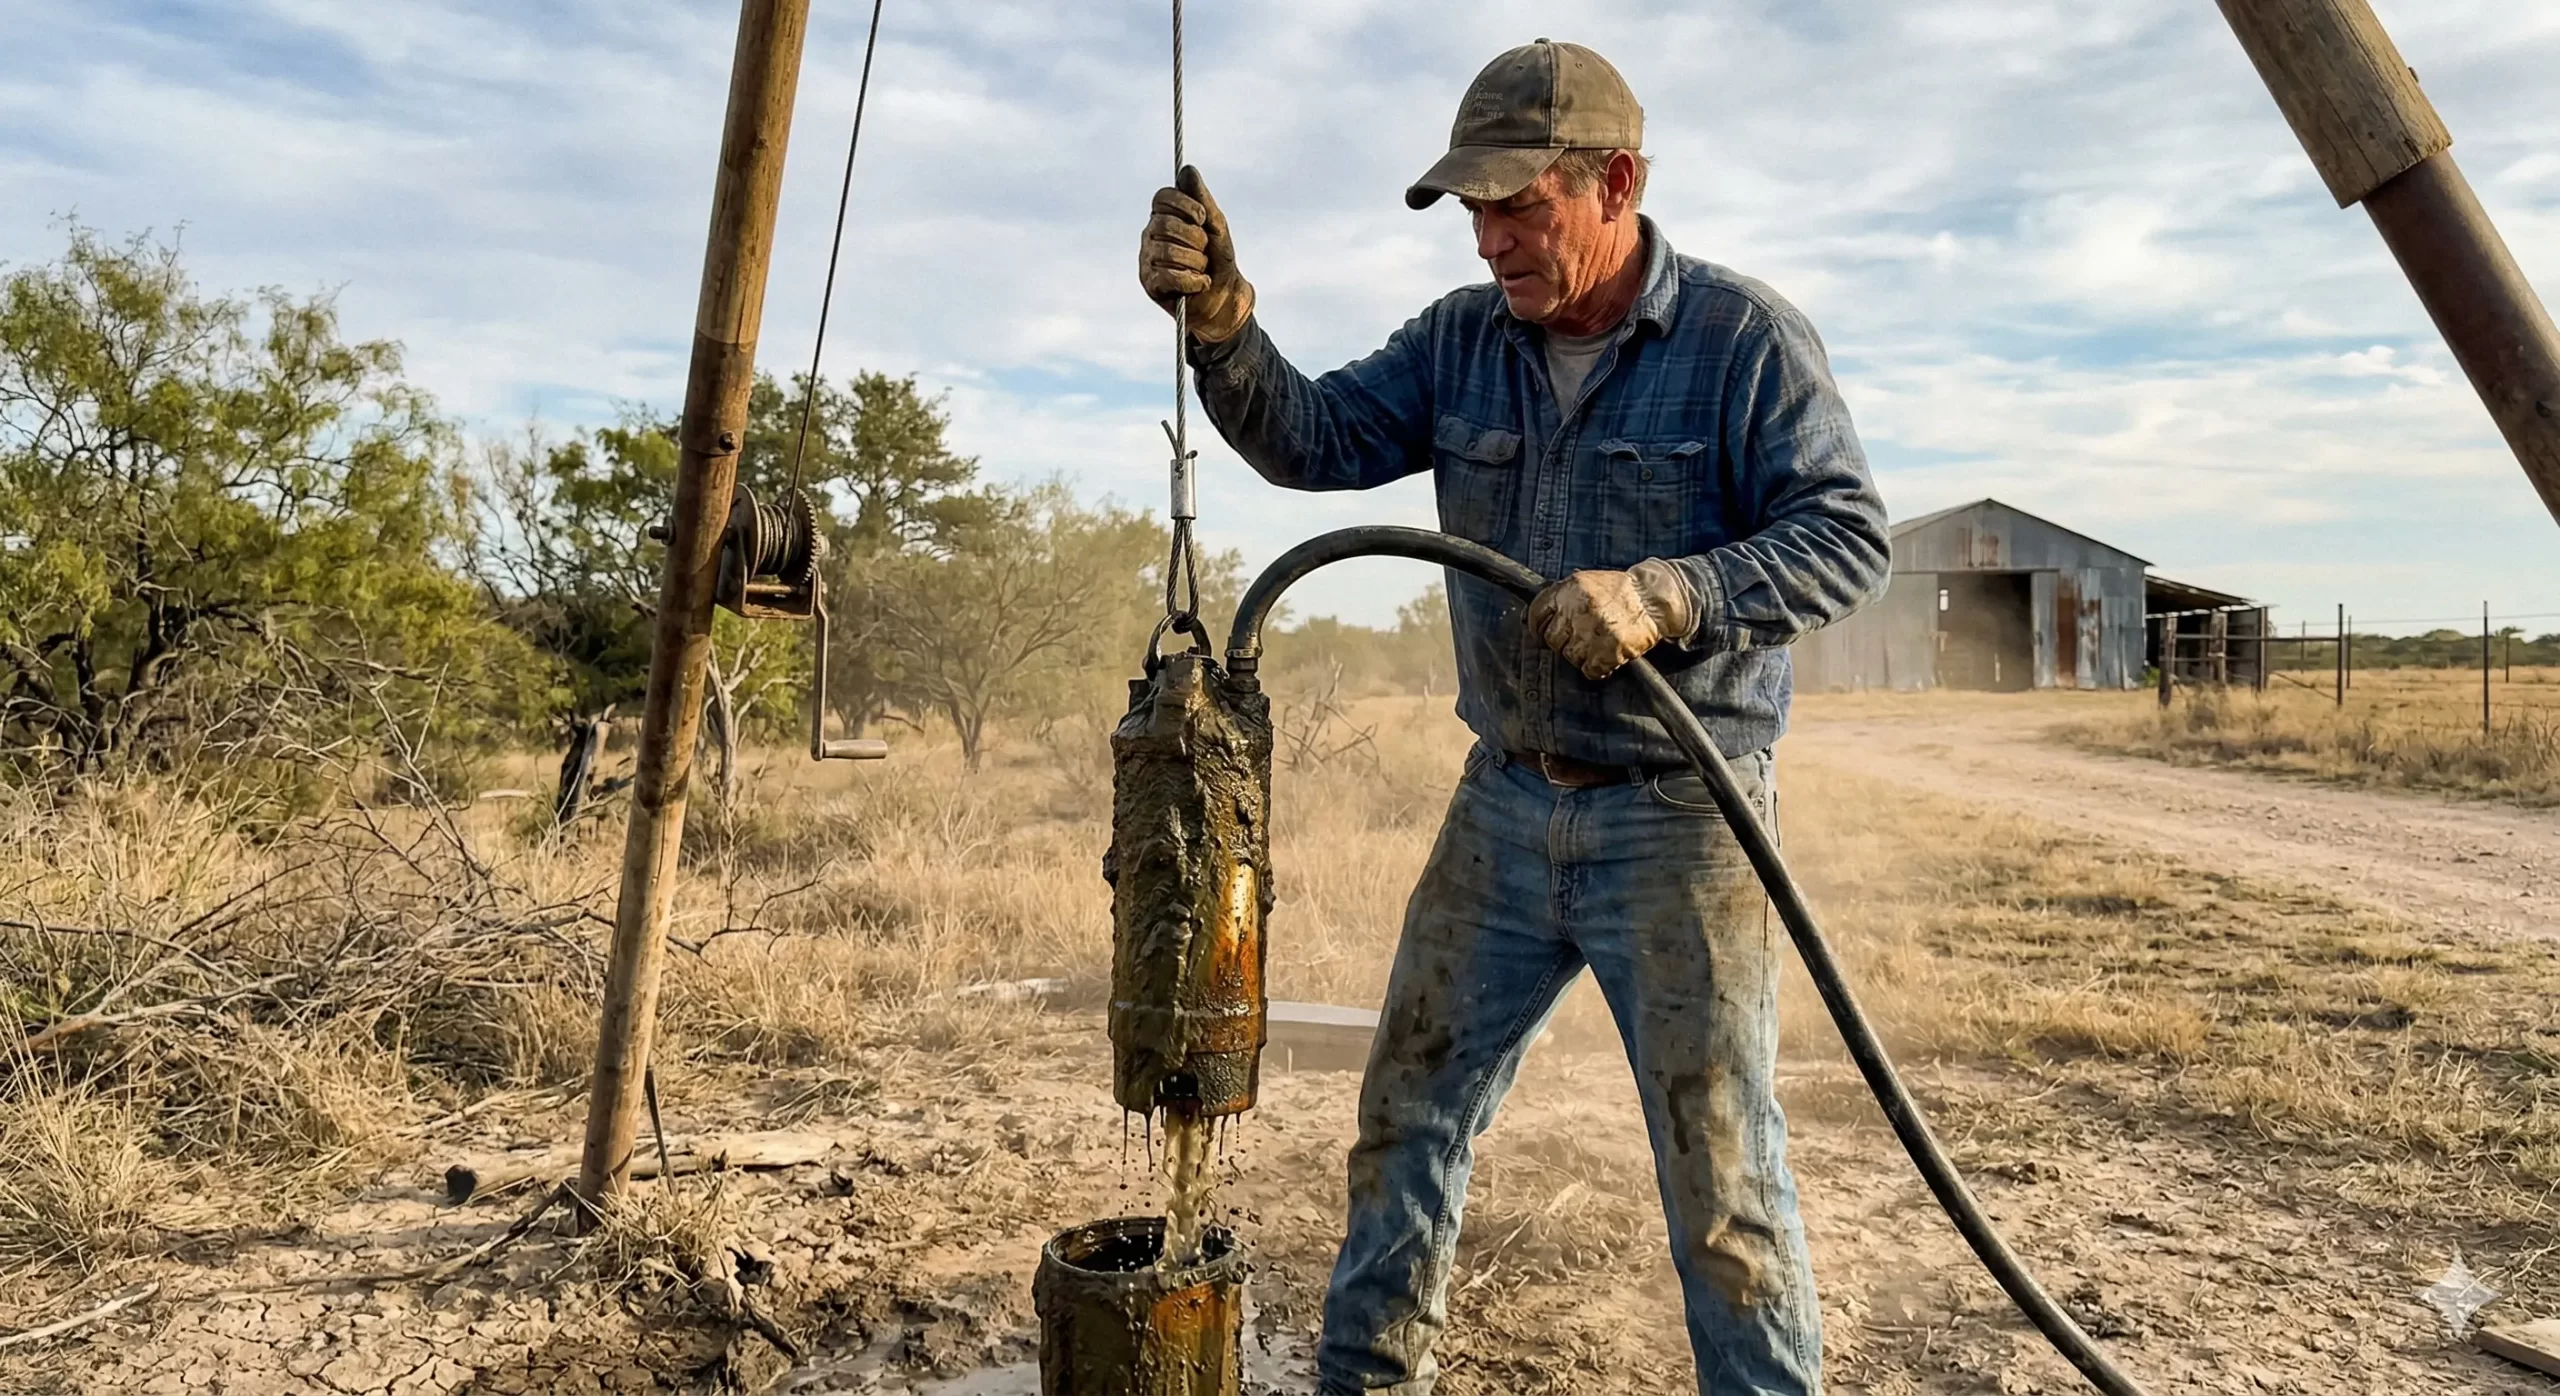
Case Study: C-345B | Location: Montgomery County, Texas
A client reported a high-level alarm and septic odor from their 7-year-old aerobic treatment unit (ATU). The property is situated on expansive clay soil, a common geological feature in this region, which necessitates an ATU with spray distribution due to the soil’s low percolation rate (less than 1 inch per hour).
Initial Diagnostics:
- Visual Inspection: The control panel alarm light was illuminated, and the audible alarm was active. The pump chamber liquid level was abnormally high, submerging the motor housing of the submersible pump. No visible signs of damage to the control panel or risers.
- Electrical Analysis: The dedicated 20-amp circuit breaker for the septic system had tripped. Upon reset, the breaker tripped again immediately upon the pump’s call to run, indicating a dead short or a seized motor. Using a clamp-on ammeter, an instantaneous current draw exceeding 50 amps was recorded before the breaker tripped, far exceeding the pump’s nameplate Full Load Amps (FLA) of 11.2A.
- Component-Level Testing: The pump was electrically disconnected at the junction box. The circuit breaker held steady when only the aerator and control panel were energized. The pump was then isolated, and a megohmmeter (megger) test was performed on the motor windings. The reading between the hot lead and ground was less than 1 megaohm, confirming a winding-to-ground fault.
Root Cause Analysis:
The submersible pump was extracted from the chamber. The cast iron volute was heavily corroded, and the intake screen was partially occluded with sludge and non-degradable solids. Disassembly revealed a complete failure of the lower mechanical seal (typically a carbon-ceramic or silicon carbide assembly). This failure allowed effluent to penetrate the oil-filled motor housing, displacing the dielectric cooling oil and causing a direct short circuit in the stator windings. The high summer ground temperatures in Texas, coupled with potential short-cycling from a previously failing float switch, likely accelerated the thermal degradation of the seal’s elastomeric components, leading to the catastrophic failure.
Resolution:
A new, appropriately sized submersible effluent pump with a superior silicon carbide seal was installed. The float switch assembly was replaced as a mandatory preventative measure. The pump chamber was pumped down to remove accumulated sludge that contributed to the initial problem. The entire system’s operational parameters, including pump cycle times and spray head pressure, were recalibrated to manufacturer specifications. The client was provided a revised maintenance schedule emphasizing biennial sludge measurement in the pump tank. Protect your property value by working with certified septic inspectors in Key West, FL.
Stop Tolerating Inadequate Maintenance Practices
The operational lifespan of an aerobic septic pump is not a fixed variable; it is a direct function of the system’s operating conditions, influent characteristics, and, most critically, the rigor of the preventative maintenance protocol. A pump operating under ideal, manufacturer-specified conditions can achieve a lifespan of 10-15 years. However, field data indicates the average lifespan is closer to 5-8 years due to widespread neglect of fundamental maintenance procedures.
Mandate Biennial Sludge and Scum Layer Measurement
The accumulation of sludge in the pump chamber is a primary catalyst for premature pump failure. When the sludge layer exceeds 8-12 inches, it can be drawn into the pump’s intake, causing accelerated wear on the impeller and volute. This abrasive slurry can also foul intake screens, starving the pump of fluid, which leads to overheating and cavitation. A core sample must be taken from the pump tank every two years using a sludge judge or similar device to measure the solids layer. If the sludge level is within 30% of the pump intake height, the tank must be pumped by a licensed professional.
Enforce Strict Effluent Filter and Screen Cleaning
Any effluent filter preceding the pump chamber or an intake screen on the pump itself must be cleaned quarterly to semi-annually. A clogged filter restricts flow to the pump, forcing it to run longer and hotter to discharge the required volume of effluent. This increased run time directly correlates to a shorter lifespan for motor windings and bearings. Documenting the pressure differential across the filter before and after cleaning provides a quantifiable metric of system health. A significant pressure drop indicates a system that is organically overloaded. Upgrading your system? Let our Rayville, LA installation experts walk you through the options.
Verify Control Panel and Float Switch Functionality Annually
The float switches are the pump’s primary control mechanism. If the ‘off’ float becomes waterlogged or fails, the pump may run continuously (run-dry condition), leading to catastrophic thermal failure. If the ‘on’ float fails, the tank can overflow, triggering the high-level alarm and potentially causing an unsanitary discharge. An annual operational test is mandatory. This involves manually lifting each float (off, on, high-level alarm) to confirm the corresponding action from the pump and control panel. The electrical contacts within the control panel relays should also be inspected for pitting or carbon tracking, which indicates excessive electrical load or short-cycling. Regular maintenance is crucial. Connect with our Corpus Christi, TX septic experts to schedule a check-up.
Verified Client Testimonials
David Chen, P.E.
⭐⭐⭐⭐⭐
“The technical precision and diagnostic rigor were unparalleled. They didn’t just replace our failed aerator; they performed a full system analysis, identified the root cause in the control panel’s timer settings, and recalibrated the entire ATU for optimal efficiency. The detailed report they provided, complete with amperage readings and pressure tests, was exactly the level of professionalism I expect. A truly engineering-focused approach to septic service.”
Dr. Maria Flores
⭐⭐⭐⭐⭐
“Our property has challenging soil conditions, and our previous septic company struggled. The team here diagnosed a TDH mismatch with our existing spray field and effluent pump. They engineered a solution involving a new pump and minor piping modifications that solved a recurring alarm issue we’ve had for years. Their understanding of fluid dynamics and wastewater chemistry is evident. Highly recommend.”
Recognize the Progression of Pump Failure
Component degradation in an aerobic septic pump is not instantaneous but follows a predictable timeline. Early detection through vigilant monitoring can prevent catastrophic failure and unsanitary surface discharge. The following timeline represents a typical pump operating under average-to-poor maintenance conditions.
- Year 1-2: Optimal Performance. The pump operates within its specified electrical (FLA) and hydraulic (GPM) parameters. Bearings are silent, seals are intact. The motor operates at a normal temperature. Routine maintenance involves only cleaning effluent screens.
- Year 3-5: Incipient Wear. Minor increases in operational noise (a faint hum or whine) may indicate initial bearing wear. The pump’s cycle time may slightly increase to discharge the same volume of water, suggesting minor impeller erosion or partial clogging. Amperage draw may increase by 5-10% from baseline. This is a critical window for preventative maintenance.
- Year 5-7: Significant Degradation. The pump becomes noticeably louder. Intermittent tripping of the circuit breaker may occur during startup, indicating high inrush current due to worn motor windings or a failing start capacitor. Seals may begin to weep, though this is not externally visible. Pump performance is visibly diminished.
- Year 7+: Imminent Failure. The pump trips the breaker frequently or immediately upon activation. A grinding noise indicates catastrophic bearing failure. An oil sheen may be visible in the pump chamber effluent, indicating a total mechanical seal breach. The pump is non-operational, leading to a high-level alarm and system backup. Replacement is unavoidable.
Cease Guesswork: Implement a Diagnostic Protocol
Troubleshooting a malfunctioning aerobic pump requires a systematic, data-driven approach. Randomly replacing parts without proper diagnosis is both inefficient and costly. Follow this engineering-grade protocol.
Step 1: Conduct a Thorough Electrical Systems Check
Before ever touching the pump, the entire electrical circuit must be verified. Using a calibrated multimeter, confirm proper voltage at the control panel’s pump terminals (typically 240V, phase-to-phase). Check for voltage drop between the panel and the pump’s junction box; a drop exceeding 3% indicates a wiring issue. With power off and locked out, check the resistance of the motor windings (phase-to-phase and phase-to-ground). A reading of infinity (OL) to ground is required; any low resistance value indicates a fatal motor short. Test the start/run capacitors with a capacitance meter to ensure they are within their marked microfarad (µF) tolerance (usually ±10%). For fast response times, get in touch with our septic professionals servicing Indian Harbour Beach, FL.
Step 2: Isolate and Evaluate Hydraulic Performance
If the electrical system is sound, the issue is likely hydraulic. Isolate the pump and disconnect it from the discharge line. Submerge it in a test basin of clean water. Measure the flow rate (GPM) directly from the pump outlet and compare it to the manufacturer’s performance curve at zero static head. If the flow is significantly below specification, the impeller is either clogged or worn. Inspect the volute and impeller for damage or obstruction from solids. A pressure gauge installed on the discharge line during normal operation can also diagnose a worn pump (low pressure) or a downstream obstruction (high pressure).
Frequently Asked Technical Questions
Can I use a standard sump pump in my aerobic system?
Absolutely not. Standard sump pumps are designed for intermittent dewatering with clear water. They lack the solids-handling capability (typically limited to 1/8″ solids) and the corrosion-resistant materials required for continuous submersion in caustic septic effluent. An aerobic system requires a purpose-built submersible effluent pump, often with a vortex or semi-open impeller, constructed from cast iron or stainless steel to withstand the harsh chemical environment and thermal loads.
What is the difference between an effluent pump and the aerator pump?
These are two functionally distinct components. The aerator pump (or air compressor) is a low-pressure, high-volume pump that injects atmospheric oxygen into the aerobic treatment chamber to sustain the microbial colony responsible for waste digestion. The effluent pump (or submersible pump) is a high-pressure, lower-volume liquid pump located in the final pump chamber. Its sole function is to dose the treated effluent from the system to the disposal area (e.g., spray heads or drip irrigation lines) once the liquid reaches a predetermined level.
Why is my alarm on but the pump seems to be working?
This condition typically points to one of several issues. First, the pump may be suffering from reduced hydraulic capacity due to a worn impeller or a partially clogged intake/discharge line; it runs, but cannot pump down the liquid level fast enough to keep up with influent, thus triggering the high-level alarm float. Second, the ‘pump off’ float switch could be failing, causing the pump not to activate until the water is high enough to trigger both the ‘on’ and ‘alarm’ floats simultaneously. Third, it could be an issue with the aerator pump, as many control panels monitor aerator function (via a pressure switch) and will trigger the main system alarm if it fails.
Does the water quality or household chemicals affect pump life?
Yes, profoundly. High concentrations of chlorine bleach, industrial solvents, or excessive water softener backwash (high salinity) can accelerate the corrosion of metallic components like the cast iron volute and fasteners. These chemicals can also degrade the elastomers (Buna-N, Viton) used in seals and gaskets, leading to premature failure. Furthermore, ‘flushable’ wipes and other non-degradable items can wrap around the impeller, causing a mechanical bind that will lead to motor burnout. The influent composition is a critical, often overlooked, factor in pump longevity.
Technically Reviewed By:
BlixBase Master Plumber Team
20+ Years Septic Industry Experience | Certified System Inspectors